Industrial Predictive Maintenance: Moving from Theory to the Shop Floor Using IIoT Data

Pierrick
•

Predictive maintenance is one of those concepts that everyone mentions, but few plant operators have actually deployed at scale. Yet it is by no means an unproven lab technology: using standard sensors, an IIoT platform, and a structured methodology, it can be phased in progressively, equipment by equipment, where it delivers the highest return.
Between the promises of artificial intelligence and the reality of a field technician conducting rounds with a clipboard, the gap remains wide across many plants. The key takeaway is that industrial predictive maintenance does not start with complex algorithms. It starts with field data. Without continuous measurement of equipment operating parameters, anomaly detection is impossible. With it, initial drift becomes visible well before functional failure occurs.
This article examines which equipment to prioritize, the physical signals to monitor, the critical integration with CMMS tools, and the practical steps to deploy DAT'Process, the DATIVE IIoT platform designed for industrial process supervision.
Corrective, preventive, or predictive: where does your plant stand?
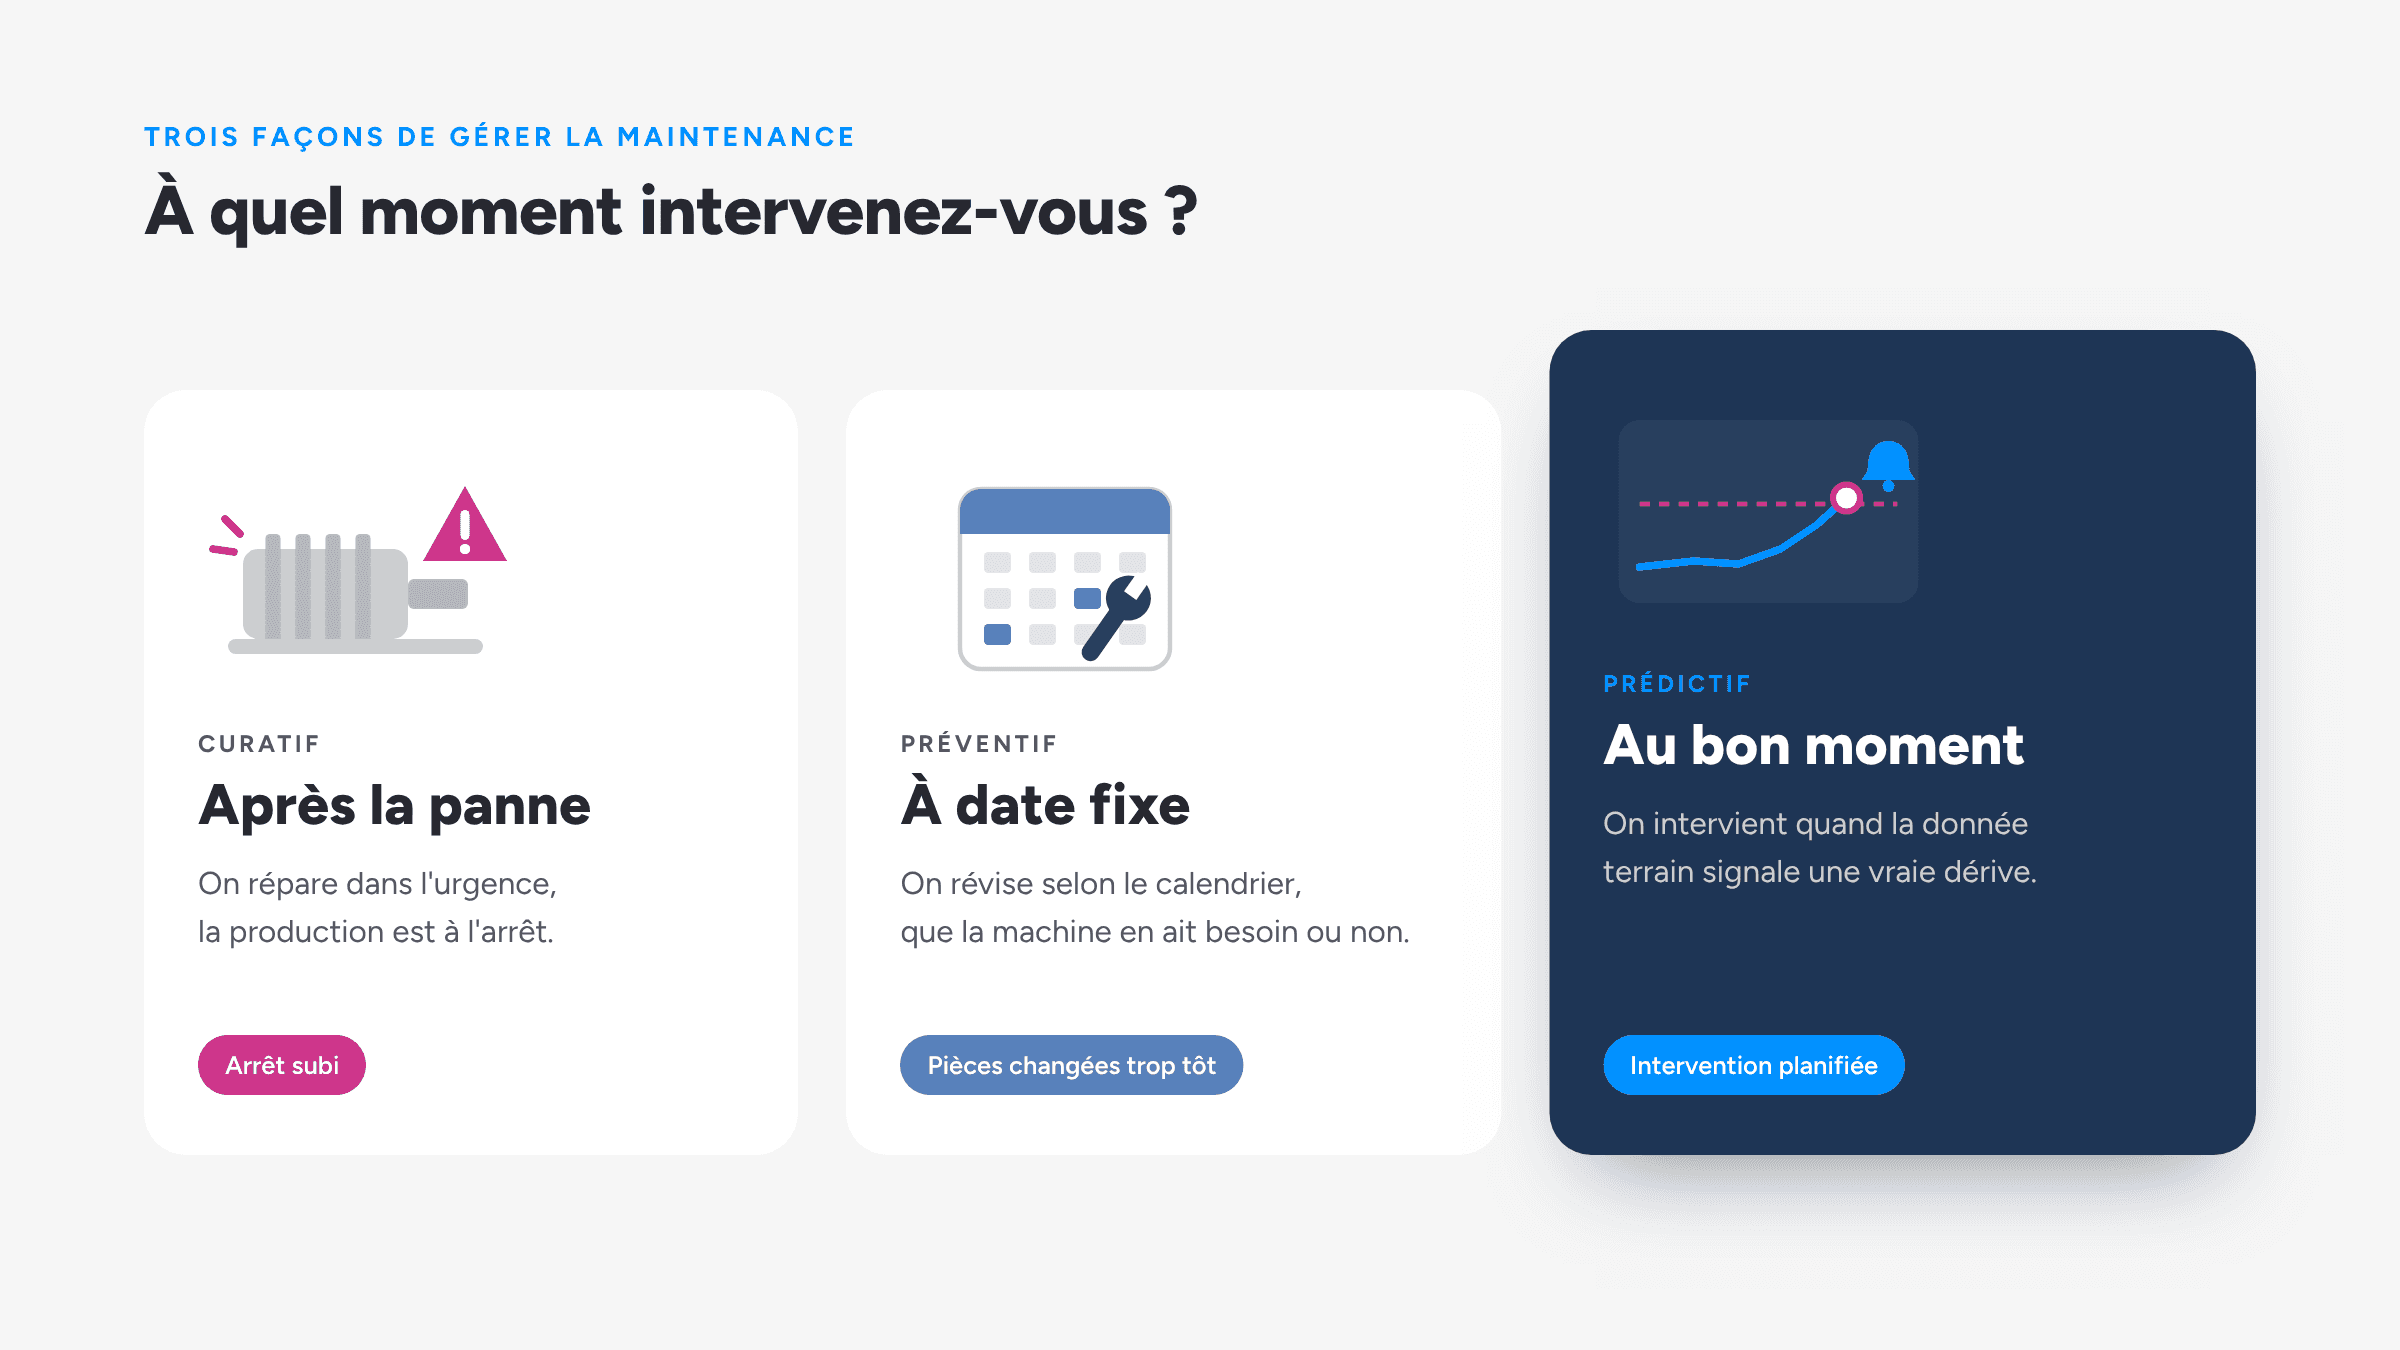
Before selecting sensors and algorithms, each asset should be mapped to one of three main maintenance strategies. A single facility almost always combines all three.
Corrective maintenance
Intervention occurs after a failure. This remains the default mode for non-critical or uninstrumented equipment. The cost per intervention is high (emergency labor, unstocked spare parts, unplanned downtime), yet it remains acceptable when the failure probability is low and its operational impact is negligible.
Preventive maintenance
Intervention is scheduled at fixed intervals, based on run hours or calendar days, regardless of actual asset condition. This is the baseline standard for critical equipment. Its two primary limitations are well documented: components still in good working condition are replaced prematurely, and defects arising between scheduled intervals go undetected.
Predictive maintenance
Intervention is triggered when field data signals actual mechanical or electrical degradation. The goal is not to switch every asset to predictive monitoring, but to apply it where the instrumentation cost is offset by the value of early detection. It relies on targeted capital expenditure rather than exhaustive plant coverage.
Which assets should be prioritized?
Not all equipment warrants predictive monitoring. Three technical criteria help determine priority:
Production impact of a failure: complete line stoppage, batch contamination, quality non-compliance, safety risk
Cost of a corrective repair: expensive components, long procurement lead times, specialized internal or outsourced labor
Progressive and measurable degradation: the asset failure presents physical precursor symptoms (vibration, temperature, power draw) well before breakdown.
In typical industrial plants, the assets meeting these criteria are air compressors, chillers, circulation pumps, large electric motors, industrial fans, and heat exchangers. These units are also frequently the facility's largest energy consumers. For compressors, our guide on industrial compressed air optimization details key operational metrics; for cooling systems, our article on industrial chillers outlines how COP drift signals fouling or refrigerant charge loss. Steam boilers follow the same operational logic.
A practical decision-making approach consists of cross-referencing failure frequency from CMMS records against the production impact for each asset. Equipment located in the upper-right quadrant of this criticality matrix represents the primary candidate list.
Technical guide available: in partnership with DIMO Maint, this guide outlines the engineering steps to transition from reactive to predictive maintenance using field data.
Field signals to monitor for early failure detection
Every mechanical or electrical failure mode produces a distinct physical signature. Predictive maintenance continuously monitors these variables to detect when values deviate from established baselines.

Vibration signatures
Vibration analysis is the primary diagnostic method for rotating machinery. Bearing wear, unbalance, and shaft misalignment emerge in the frequency spectrum weeks before functional failure. Accelerometers mounted on bearing housings transmit operational data to DAT'Process, which tracks overall vibration levels and triggers alarms when thresholds are exceeded. Thresholds can initially be mapped to ISO 20816 severity zones and subsequently calibrated using machine-specific operating history.

Operating temperatures
An abnormal temperature increase across a bearing, motor winding, or cooling circuit is often the first measurable indicator of mechanical friction or lubrication breakdown. Non-intrusive surface sensors, installed without process downtime, enable continuous thermal tracking.
Power consumption and current profiles
An electric motor showing steadily increasing current draw under a constant mechanical load typically indicates developing mechanical resistance. By correlating active power with operating parameters, DAT'Process separates underlying mechanical drift from standard load fluctuations. This method is equally applicable to locating compressed air leaks: a compressor operating longer duty cycles to meet unchanged plant demand indicates downstream distribution losses.
Asset-specific process variables
On industrial chillers, monitoring COP alongside suction pressure highlights refrigerant undercharge or heat exchanger fouling. On air compressors, tracking loaded versus unloaded cycles and discharge temperature reveals valve wear or separator element clogging. Each equipment class features dedicated operational metrics configured within DAT'Process based on plant operating conditions.
Field data acquisition: sensors, connectivity, and network security
Predictive maintenance initiatives rarely fail due to analytical complexity. They typically fail because data is missing, poorly timestamped, or trapped in disconnected silos. Three core engineering aspects must be addressed during initial scoping.
Instrumenting without process disruption. On existing brownfield assets, most required parameters can be acquired via retrofit sensors: magnetic-mount accelerometers, surface temperature probes, and split-core current transformers. When PLCs already capture these points, the IIoT platform retrieves the data directly over standard industrial protocols, avoiding redundant instrumentation.
Selecting appropriate network connectivity. Across large sites or complex physical layouts, LoRa technology enables the deployment of battery-powered sensors over a private network, minimizing cabling infrastructure. This solves a major technical challenge in industrial IoT: reliably collecting edge data from disparate, legacy equipment.
Securing data architecture. Connecting operational technology (OT) to supervisory systems requires robust network segmentation and strict data integrity controls. Our industrial cybersecurity framework details DATIVE's technical architecture, developed in coordination with N-CyP, the cybersecurity subsidiary of the Gérard Perrier Industrie Group. For high-constraint plants, our case study on a SEVESO upper-tier site details how HSE requirements, cybersecurity standards (such as NIS 2), and production uptime are maintained simultaneously.
Predictive maintenance and energy performance: a shared data layer
An operational reality often overlooked: priority predictive maintenance assets are almost always the plant's largest consumers of electrical and thermal energy. A worn compressor, a fouled heat exchanger, or a misaligned motor draws excess power long before mechanical breakdown. Energy drift is frequently the earliest indicator of mechanical degradation.
Sharing instrumentation infrastructure between maintenance and energy monitoring improves overall project ROI. Power consumption data gathered for asset health also feeds energy management workflows within DAT'Power, and vice versa. Sites that have already deployed a metering plan or an Energy Management System already possess the foundational data layer.
CEE funding mechanisms. In France, standardized fiche IND-UT-134 allows industrial sites to leverage CEE (Energy Savings Certificates) to subsidize systems that measure energy performance indicators across defined utilities (compressed air, refrigeration, pumping systems). When energy instrumentation on compressors or chillers simultaneously feeds predictive maintenance workflows, capital expenditures can be partially covered, subject to technical eligibility and compliance with applicable standard requirements.
Financial assessment: calculate potential energy savings, estimated payback period, and applicable CEE subsidy amounts.
Integrating supervision with CMMS to close the operational loop
Anomaly detection provides operational value only if it triggers a clear maintenance action. DAT'Process interfaces directly with CMMS platforms to automatically generate work orders when operational thresholds are breached. The maintenance technician receives full event context: signal trend history, baseline deviation, and previous intervention logs. This ensures field teams arrive with the correct diagnostic insight and replacement parts.

Following the intervention, closing the work order verifies whether operating indicators have returned to nominal values. Each detection-intervention-verification cycle enriches asset history, refining detection models and threshold accuracy over time. We detail this data integration in our article CMMS and IIoT supervision: integrating maintenance workflows with industrial monitoring, covering our technical integration with DIMO Maint.
Deployment roadmap: industrial predictive maintenance in four steps
Deploying predictive maintenance across an industrial plant is an iterative process of continuous operational improvement, not a single monolithic deployment.
Prioritize. Target three to five critical assets using the failure frequency versus production impact matrix, cross-checked against CMMS records.
Instrument. Install sensors aligned with the specific failure modes of those machines (vibration, temperature, current, process variables) and route telemetry to the platform.
Establish the baseline. Acquire several weeks of steady-state operational data to define normal operating profiles across various load conditions and operating regimes.
Alert, intervene, scale. Configure alert thresholds, route triggers into the CMMS, validate operational gains, and expand coverage to secondary assets as operational teams integrate the tooling.
Once this verified data layer is established, advanced tools like machine learning can be effectively applied. As discussed in our article on IIoT, data, and AI, artificial intelligence cannot substitute for reliable field data; it depends entirely on it.
For original equipment manufacturers (OEMs) seeking to integrate predictive monitoring into their equipment: DAT'Machine enables remote fleet monitoring, early mechanical fault identification, and connected service contract delivery.
Summary: predictive maintenance as a methodological standard
Predictive maintenance is neither an exclusive tool for large enterprises nor a multi-year software R&D effort. It is an engineering process: isolate critical assets, capture reliable physical signals, integrate alerts with CMMS workflows, and validate results after each intervention. By aligning instrumentation with energy management, plants also reduce operating expenses and can leverage regulatory mechanisms like CEE.
Industrial sites achieving the highest uptime do not instrument everything at once. They target high-criticality assets first, quantify performance gains, and scale systematically. Review how other facilities have deployed this framework in our case studies.
Planning a predictive maintenance deployment? Our technical team assists in asset prioritization, sensor selection, and expected ROI modeling using DAT'Process.